
- 팔로우
- 팔로우
- 팔로우
- 팔로우
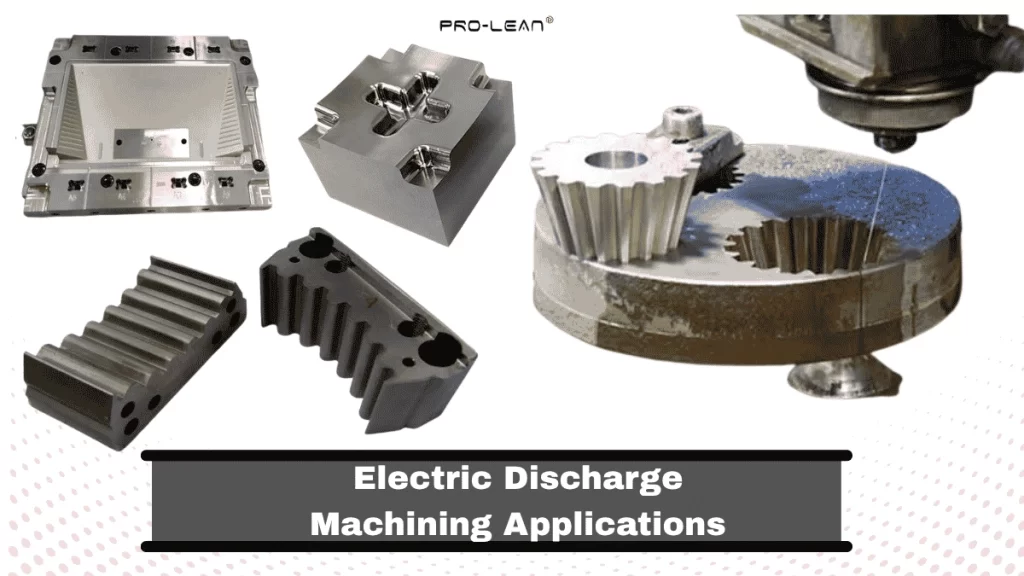
Electric Discharge Machining Applications
방전 가공 (EDM) cuts, shapes, and micro-drills on electrically conductive materials using a controlled discharge under a dielectric medium. It is chosen when conventional cutting is limited by high hardness and intricate geometries, as EDM removes material through controlled electrical discharges and can machine hardened materials and delicate features. Mold & die tooling, fuel-injectors, precision gears, surgical instruments, and turbine blades are common EDM applications.
EDM is used to cut deep holes, cavities, sharp corners, curved holes, slots, ribs, and various micro-features that are challenging or impossible to create with traditional CNC machining processes. So, it has extensive use in precision machining across industries, enabling complex parts, tight tolerances, fine finishes, and hardened-metal shaping.
The upcoming sections will elaborate on electrical discharge machining applications, process mechanism, and how you can leverage this technology for your project.
Electrical Discharge Machining: How Does This Non-Contact Machining Work?
Working of EDM in manufacturing
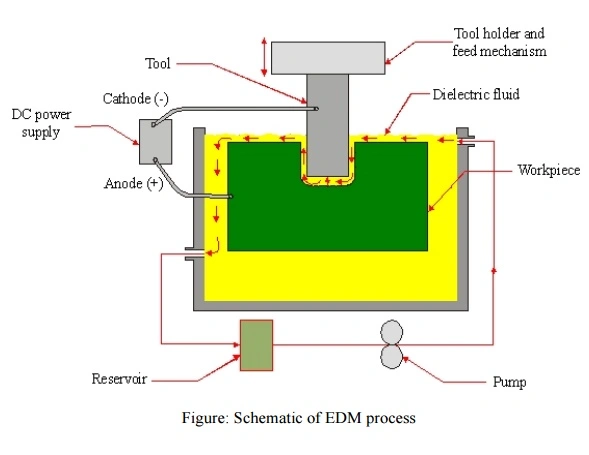
Electrical Discharge Machining (EDM) is a non-conventional subtractive manufacturing process, in which a tool (electrode/wire) removes the material from conductive workpieces using controlled electric sparks inside a dielectric medium. This means there is no direct contact between the electrode and the workpiece. It is far less sensitive to workpiece hardness than conventional cutting, but machinability still depends on electrical and thermal properties, material composition, flushing, and process parameters. y.
As current passes through the electrode, it creates a gap with the workpiece and produces extreme heat (plasma), which melts and erodes the material. The discharge plasma channel temperature can be ~ 20,000 ° C or even higher. This high temperature also brings the electric discharge safety 문제.
Let’s look at the components involved in the electrical discharge machining process.
- 펄스 생성기: It times and shapes the voltage/current pulse
- 전극: Acts as a tool, which is shaped as a cavity’s inverse or a continuous wire.
- Servo Feed & Gap Control Systems: These components analyze gap-voltage feedback and reposition the electrode.
- 유전체 유체: The dielectric initially insulates the electrode gap; under a sufficiently strong electric field, it ionizes and forms a conductive plasma channel. It also cools the machining zone and flushes away eroded debris.
- Pump and Filter: These are used to reuse the dielectric fluid and remove the impurities from the fluid before passing it back into the system.
How is an Electric Spark Generated in EDM?
As the electrode approaches the workpiece, the pulsed power supply raises the potential difference across the narrow gap. The electric field ionizes the dielectric fluid. Electrons emitted from the cathode accelerate through the gap and collide with neutral dielectric molecules. So, it loses electrons and ions. Once the ion/electron density is high enough, the gap turns conductive, forming a narrow plasma channel, called a “spark”.
전기방전가공의 종류
Sinker EDM, Wire EDM, Hole Drilling EDM, and Small Hole Drilling EDM are the main types of electric discharge machining.
Die-sinking or Sinker EDM
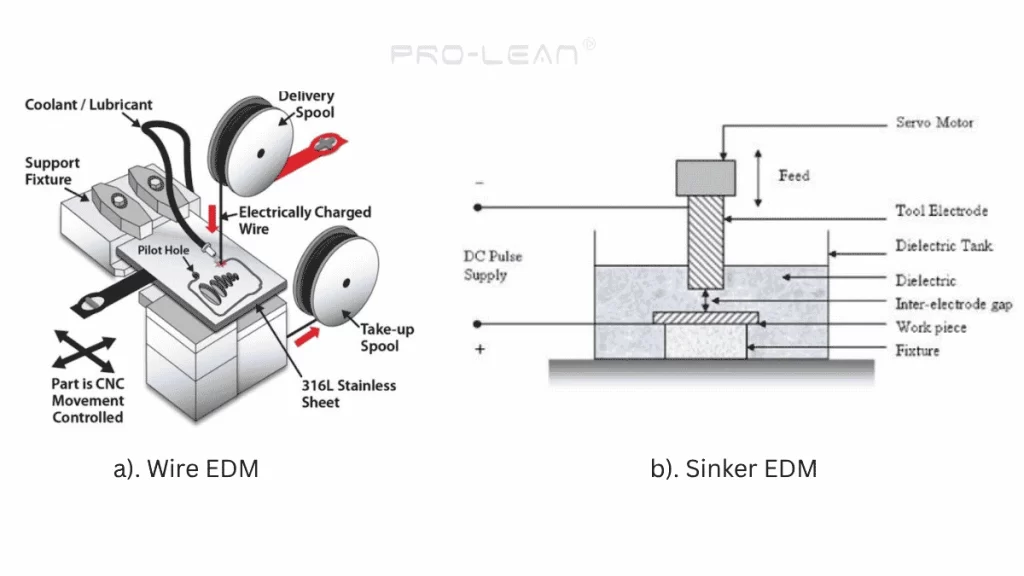
Wire vs Sinker EDM
The Sinker EDM method uses a copper or graphite electrode that perfectly matches the desired shape/features, which then sinks into the workpiece. This means that, first, you need a custom electrode with a designed shape.
As the electrode is plunged into the workpiece, it produces the negative geometry. A ram head pushes the electrode into the workpiece, which is submerged in dielectric fluid.
적합한 응용 프로그램 : Profile, cavity, blind features, complex 3D forms in dies, molds, and industrial components.
와이어 방전 가공
As the name suggests, wire EDM uses a continuously moving “ 와이어 전극 ” made from copper, brass, or zinc-coated brass. The wire electrode is fed into the material to cut complex profiles and contours, following the CAD model.
적합한 응용 프로그램 : Profiling and contouring in stamping dies, gears, and extrusion tooling.
홀 드릴링 EDM
This type of EDM is used to create narrow, deep holes. A hollow tubular electrode penetrates the workpiece while supplying the dielectric solution itself to remove the eroded material.
적합한 응용 프로그램 : Fuel injectors, heat sinks, hypodermic tube features, endoscopic components, etc.
Small Hole-drilling EDM
Small Hole-drilling EDM or fast hole EDM involves using a hollow tubular electrode to erode small, high aspect ratio holes in conductive materials. They can create holes with a diameter smaller than 0.3 mm while maintaining an L/D ratio of 15:1 or higher. Meanwhile, specialized micro-EDM creates holes with diameters of < 0.1 mm and an L/D ratio> 30: 1.
적합한 응용 프로그램 : Drug delivery systems, silicon wafers, fuel injectors with micro-scale spray holes, and optical slits.
Next, let’s discuss the electric discharge machining applications across industries one by one.
Electric Discharge Machining Applications in Medical Device Manufacturing
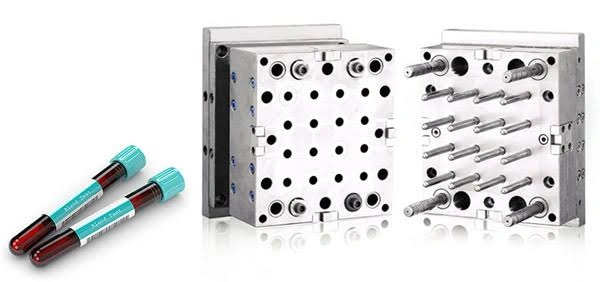
EDM medical applications
Medical device manufacturing requires micro-machining and tight precision, as it directly impacts diagnostic accuracy, patient health, and custom solutions. So, EDM is used in a range of medical manufacturing, from patient-specific implants to diagnostic equipment components and surgical tools.
EDM works well with fully hardened and biocompatible materials, such as titanium alloys, stainless steels, and cobalt-chrome. It cuts sharp corners and produces microscale features (slots with ~0.1 mm width,> 150 mm deep holes, etc.), which are essential in medical manufacturing.
애플리케이션 예제 :
- Cardiovascular stents of titanium, 316L stainless steel, and nitinol.
- Hip and Knee implants with surface texturing
- Surgical blades, cannulas, and forceps with sharp cutting edges & complex profiles
- 치과 용 임플란트
- Drug delivery devices with micro-holes ( ⌀ < 0.3 mm)
- 골판
Specific Case-Example:
EDM machining manufacturers 사용 die-sink EDM method for implantable devices (cardiovascular stents, AISI 316L). Applying an optimal pulse current of 1.5 A/45 µs [ 1 ] for this ensures the desired recast thickness, crater size, and surface finish.
Electric Discharge Machining Applications in the Automotive Industry
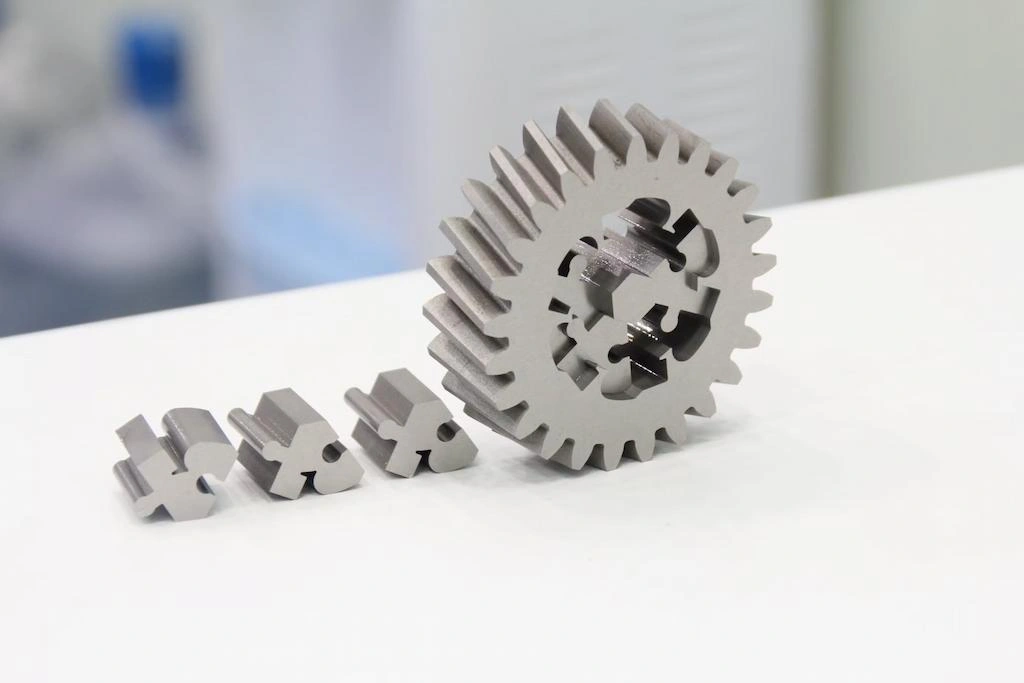
EDM machined gears for automotive
The electrical discharge machining process is used in the automotive industry either to create components with critical & micro features or for molds and dies that produce auto parts in large volumes. For instance, micro-hole drilling in fuel injectors and injection molds for dashboard molding.
Gearbox components, valve guides, nozzle rings, and similar parts require micro-precision and fine detailing, which are difficult to achieve with CNC milling and drilling. So, EDM is used to meet these requirements.
- Spray holes in the fuel-injector nozzle with a high aspect ratio
- Injector needle valves and seats with tight sealing tolerance
- Helical and bevel gear cavities
- Turbocharger components with fine clearances
- Electric connectors & micro-switches
- Stamping dies for body panels
- Extrusion dies for structural aluminum profiles
- Injection molding dies for automotive plastic components
Last month, we received a “ Diesel Fuel Injector Nozzle Prototype ” design via our online platform. The hole diameter was under 140 µm, and the exit needed to be wider than the entrance to disperse the fuel into a fan-shaped spray. Our engineers use laser pilot-hole drilling, followed by EDM small-hole drilling. The client said this helps to improve fuel efficiency by ~1.2 % during the initial testing phase.
지금 프로린을 사용해 보세요!
Electric Discharge Machining Applications in Die and Mold Tooling
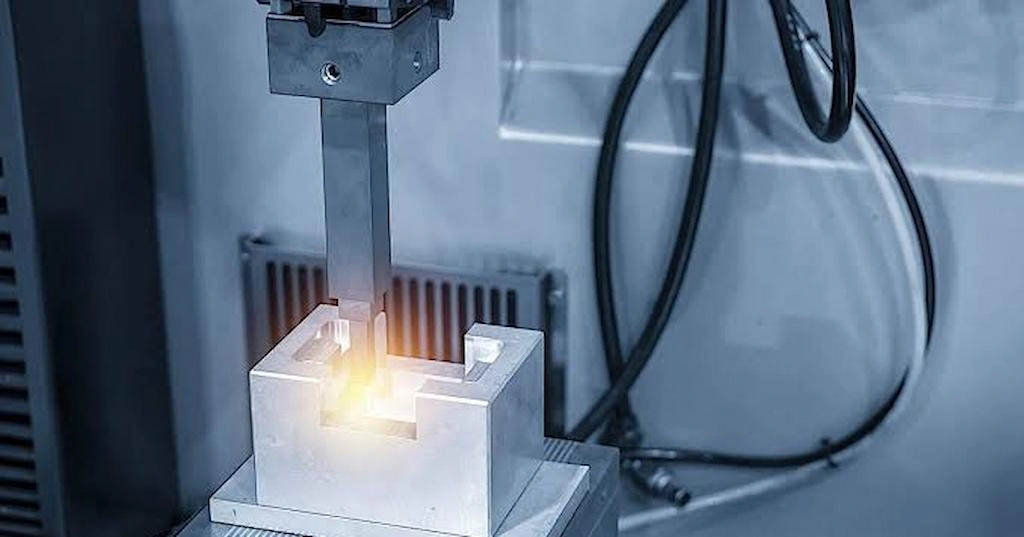
EDM die tooling
The 방전 가공 공정 has extensive applications in the manufacturing of dies, molds, tools, and fixtures. This is due to its capabilities for complex profiling, micro-machining, hardened-material machining, deep-cavity & channel creation, and dimensional accuracy.
EDM does not involve cutting forces as in traditional machining; instead, it uses a spark discharge to remove material from the workpiece. So, it can directly cut fragile, thin-walled sections, long cavities, narrow slots, and other features with micro-detailing. Additionally, tooling materials such as D2, H13, and carbides can be cut directly with electrodes or wires.
Sinker EDM offers ~ ± 0.025 mm positioning accuracy and a finish quality of 0.1 µm Ra (even lower with specialized machines). They can create precisely placed holes on die & mold tooling for ejector, venting, and cooling.
- Injection mold (cores and cavities)
- Ejector-pin holes and beveled cooling holes in molds
- 3D impression cavities in forging dies
- Sheet metal forming dies (Progressive and trim dies)
- Stamping punch & die set
- Tread blocks and sipes for tire mold segments
- EDM electrodes for subsequent sinker EDM work
- Custom fixtures for lathes and CNC mills.
- Go/no-go gauges and profile gauges
- Gauge inserts and inspection templates
Electric Discharge Machining Applications in the Aerospace Industry
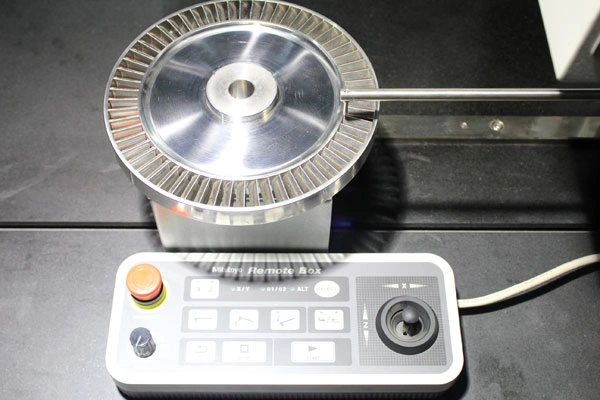
Aerospace EDM machining
EDM produces various aerospace components from hard, heat-resistant, high-performance metals & alloys, such as Ti-6Al-4V, Ti-17, Inconel, tungsten, and Waspaloy . Electric discharge machining is used for cooling channels in turbines, honeycomb seals, and intricate engine geometries.
EDM in manufacturing aerospace components maintains tolerances in microns, minimizes heat-affected zones, and eliminates work-hardening risks, which are critical for precision and aircraft safety.
Furthermore, EDM complies with safety and quality standards for aerospace manufacturing, including AS9100, SAE AS7116/3 예산 및 MIL-STD-2175 .
- Small, deep, and angled holes on turbine blades
- Fir-tree slot profiles in turbine discs
- Honeycomb seals in jet engine casings
- Fuel nozzle swirlers
- Complex thin-wall airfoils
- Structural sections and complex profiles in landing gear components
- 유압 액추에이터
- 밸브 부품
- Titanium brackets & mounts for satellites
Electric Discharge Machining Applications in Electronics and Semiconductors
In electronics and the semiconductor industry, the need for micro-level components has grown, along with the use of hard materials such as silicon carbide and gallium nitride. EDM can machine heavily doped SiC and GaN. Micro-switches, connectors, sensor housings, test sockets, and probe cards are a few examples.
Because EDM does not involve shear cutting, it preserves the fragile micro-connector geometry of semiconductor components. Consequently, the burr-free machining allows the shaping of fine-pitch electronic components.
- Fine-pitch micro-connector components
- Semiconductor process-equipment fixtures
- Probe card test needles
- Wafer testing parts/ wafer slicing
- MEMS and inkjet printheads
- IC-test sockets
- 스퍼터링 타겟
EDM Applications in Defense Manufacturing
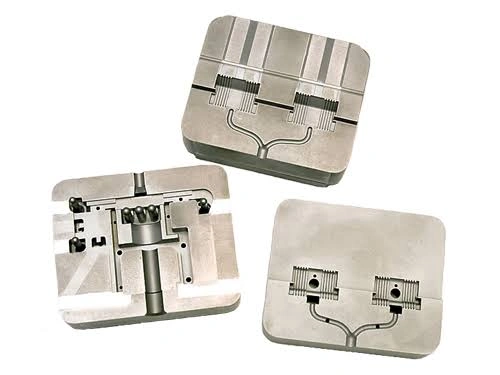
EDM applications in electronics
Precision and detailing are crucial in the manufacturing of defense equipment and components, so EDM is used to produce components for missile systems, radars, weapons, and military aircraft. Additionally, EDM is a good choice for precision machining of high-performance alloys that can withstand extreme pressure and heat.
The key reasons why EDM in the manufacturing of defense components is valued are: the ability to shape and profile hardened aerospace alloys, near-zero cutting force & surface integrity, dimensional accuracy, and small-hole drilling.
- Avionics housings and precision connector components
- Gyroscope flexures
- Space-propulsion class hardware
- Aero-engine nozzle-guide-vane
- 미사일 유도 구성 요소
- Precision satellite components
EDM Applications in Hard Materials Machining
As mentioned before, EDM can cut, shape, and drill hard, heat-treated materials (such as cobalt-bonded tungsten carbide, ~ >70 HRC ); the basic requirement is that the workpiece be electrically conductive.
A conventional CNC machining process, such as milling, uses the shear-cutting method and therefore struggles to machine hard materials due to rapid tool wear. But EDM works well as it removes material by controlled electric sparks. Unlike tool-reach issues in milling or drilling, EDM uses an electrode/wires and can drill long, deep holes precisely.
Let’s look at some hard metals/alloys that can be used in the electrical discharge machining process.
소스
Hardness (~ Approx. HRC)
어플리케이션
AISI H13 공구강
45-55
Dies, inserts, complex cavities
D2 공구강
55-62
Punches, dies, profiles
M2 고속철
60-65
Cutting-tools & Dies
Maraging steel (e.g., M300)
50-55
Thin flexures and aerospace parts
인코넬 718
35-50
터빈 부품
니켈 기반 초합금
30–50 +
터빈 블레이드/베인
티타늄 합금(Ti-6Al-4V)
30-40
Aerospace/defense components
Cemented carbide (WC–Co)
> 70
Dies, punches, and tooling
EDM 가공 서비스 Based on Your CAD Design
At Boda, we excel in machining small, intricate, and detailed features for your parts with tolerances as low as ±0.004 mm . We can handle 30+ hard and difficult materials, including tool steels, hardened steels, titanium alloys, Inconel, and carbides.
At our factory, we have wire EDM, Die-sinker EDM, Hole drilling EDM, and micro-EDM equipment that can be used for custom die & mold tooling production and a variety of industrial components. Our EDM services can also deliver a 혼성 접근법 . If workpieces are processable with milling, turning, drilling, or other methods, we combine them with EDM. CNC machining handles fast bulk material removal and accessible geometry. Then, EDM is used for hard, intricate, small, deep, or force-sensitive features.
에 견적을 원하시면 바로 연락주세요 for your EDM machining design, upload your CAD file and specify the requirements. Our engineers will review your design and provide you with an estimation with DFM feedback.
Electric Discharge Machining Applications
방전 가공 (EDM) cuts, shapes, and micro-drills on electrically conductive materials using a controlled discharge under a dielectric medium. It is chosen when conventional cutting is limited by high hardness and intricate geometries, as EDM removes material through controlled electrical discharges and can machine hardened materials and delicate features. Mold & die tooling, fuel-injectors, precision gears, surgical instruments, and turbine blades are common EDM applications.
EDM is used to cut deep holes, cavities, sharp corners, curved holes, slots, ribs, and various micro-features that are challenging or impossible to create with traditional CNC machining processes. So, it has extensive use in precision machining across industries, enabling complex parts, tight tolerances, fine finishes, and hardened-metal shaping.
The upcoming sections will elaborate on electrical discharge machining applications, process mechanism, and how you can leverage this technology for your project.
Electrical Discharge Machining: How Does This Non-Contact Machining Work?
Working of EDM in manufacturing
Electrical Discharge Machining (EDM) is a non-conventional subtractive manufacturing process, in which a tool (electrode/wire) removes the material from conductive workpieces using controlled electric sparks inside a dielectric medium. This means there is no direct contact between the electrode and the workpiece. It is far less sensitive to workpiece hardness than conventional cutting, but machinability still depends on electrical and thermal properties, material composition, flushing, and process parameters. y.
As current passes through the electrode, it creates a gap with the workpiece and produces extreme heat (plasma), which melts and erodes the material. The discharge plasma channel temperature can be ~ 20,000 ° C or even higher. This high temperature also brings the electric discharge safety 문제.
Let’s look at the components involved in the electrical discharge machining process.
- 펄스 생성기: It times and shapes the voltage/current pulse
- 전극: Acts as a tool, which is shaped as a cavity’s inverse or a continuous wire.
- Servo Feed & Gap Control Systems: These components analyze gap-voltage feedback and reposition the electrode.
- 유전체 유체: The dielectric initially insulates the electrode gap; under a sufficiently strong electric field, it ionizes and forms a conductive plasma channel. It also cools the machining zone and flushes away eroded debris.
- Pump and Filter: These are used to reuse the dielectric fluid and remove the impurities from the fluid before passing it back into the system.
How is an Electric Spark Generated in EDM?
As the electrode approaches the workpiece, the pulsed power supply raises the potential difference across the narrow gap. The electric field ionizes the dielectric fluid. Electrons emitted from the cathode accelerate through the gap and collide with neutral dielectric molecules. So, it loses electrons and ions. Once the ion/electron density is high enough, the gap turns conductive, forming a narrow plasma channel, called a “spark”.
전기방전가공의 종류
Sinker EDM, Wire EDM, Hole Drilling EDM, and Small Hole Drilling EDM are the main types of electric discharge machining.
Die-sinking or Sinker EDM
Wire vs Sinker EDM
The Sinker EDM method uses a copper or graphite electrode that perfectly matches the desired shape/features, which then sinks into the workpiece. This means that, first, you need a custom electrode with a designed shape.
As the electrode is plunged into the workpiece, it produces the negative geometry. A ram head pushes the electrode into the workpiece, which is submerged in dielectric fluid.
적합한 응용 프로그램 : Profile, cavity, blind features, complex 3D forms in dies, molds, and industrial components.
와이어 방전 가공
As the name suggests, wire EDM uses a continuously moving “ 와이어 전극 ” made from copper, brass, or zinc-coated brass. The wire electrode is fed into the material to cut complex profiles and contours, following the CAD model.
적합한 응용 프로그램 : Profiling and contouring in stamping dies, gears, and extrusion tooling.
홀 드릴링 EDM
This type of EDM is used to create narrow, deep holes. A hollow tubular electrode penetrates the workpiece while supplying the dielectric solution itself to remove the eroded material.
적합한 응용 프로그램 : Fuel injectors, heat sinks, hypodermic tube features, endoscopic components, etc.
Small Hole-drilling EDM
Small Hole-drilling EDM or fast hole EDM involves using a hollow tubular electrode to erode small, high aspect ratio holes in conductive materials. They can create holes with a diameter smaller than 0.3 mm while maintaining an L/D ratio of 15:1 or higher. Meanwhile, specialized micro-EDM creates holes with diameters of < 0.1 mm and an L/D ratio> 30: 1.
적합한 응용 프로그램 : Drug delivery systems, silicon wafers, fuel injectors with micro-scale spray holes, and optical slits.
Next, let’s discuss the electric discharge machining applications across industries one by one.
Electric Discharge Machining Applications in Medical Device Manufacturing
EDM medical applications
Medical device manufacturing requires micro-machining and tight precision, as it directly impacts diagnostic accuracy, patient health, and custom solutions. So, EDM is used in a range of medical manufacturing, from patient-specific implants to diagnostic equipment components and surgical tools.
EDM works well with fully hardened and biocompatible materials, such as titanium alloys, stainless steels, and cobalt-chrome. It cuts sharp corners and produces microscale features (slots with ~0.1 mm width,> 150 mm deep holes, etc.), which are essential in medical manufacturing.
애플리케이션 예제 :
- Cardiovascular stents of titanium, 316L stainless steel, and nitinol.
- Hip and Knee implants with surface texturing
- Surgical blades, cannulas, and forceps with sharp cutting edges & complex profiles
- 치과 용 임플란트
- Drug delivery devices with micro-holes ( ⌀ < 0.3 mm)
- 골판
Specific Case-Example:
EDM machining manufacturers 사용 die-sink EDM method for implantable devices (cardiovascular stents, AISI 316L). Applying an optimal pulse current of 1.5 A/45 µs [ 1 ] for this ensures the desired recast thickness, crater size, and surface finish.
Electric Discharge Machining Applications in the Automotive Industry
EDM machined gears for automotive
The electrical discharge machining process is used in the automotive industry either to create components with critical & micro features or for molds and dies that produce auto parts in large volumes. For instance, micro-hole drilling in fuel injectors and injection molds for dashboard molding.
Gearbox components, valve guides, nozzle rings, and similar parts require micro-precision and fine detailing, which are difficult to achieve with CNC milling and drilling. So, EDM is used to meet these requirements.
- Spray holes in the fuel-injector nozzle with a high aspect ratio
- Injector needle valves and seats with tight sealing tolerance
- Helical and bevel gear cavities
- Turbocharger components with fine clearances
- Electric connectors & micro-switches
- Stamping dies for body panels
- Extrusion dies for structural aluminum profiles
- Injection molding dies for automotive plastic components
Last month, we received a “ Diesel Fuel Injector Nozzle Prototype ” design via our online platform. The hole diameter was under 140 µm, and the exit needed to be wider than the entrance to disperse the fuel into a fan-shaped spray. Our engineers use laser pilot-hole drilling, followed by EDM small-hole drilling. The client said this helps to improve fuel efficiency by ~1.2 % during the initial testing phase.
지금 프로린을 사용해 보세요!
Electric Discharge Machining Applications in Die and Mold Tooling
EDM die tooling
The 방전 가공 공정 has extensive applications in the manufacturing of dies, molds, tools, and fixtures. This is due to its capabilities for complex profiling, micro-machining, hardened-material machining, deep-cavity & channel creation, and dimensional accuracy.
EDM does not involve cutting forces as in traditional machining; instead, it uses a spark discharge to remove material from the workpiece. So, it can directly cut fragile, thin-walled sections, long cavities, narrow slots, and other features with micro-detailing. Additionally, tooling materials such as D2, H13, and carbides can be cut directly with electrodes or wires.
Sinker EDM offers ~ ± 0.025 mm positioning accuracy and a finish quality of 0.1 µm Ra (even lower with specialized machines). They can create precisely placed holes on die & mold tooling for ejector, venting, and cooling.
애플리케이션 예제 :
- Injection mold (cores and cavities)
- Ejector-pin holes and beveled cooling holes in molds
- 3D impression cavities in forging dies
- Sheet metal forming dies (Progressive and trim dies)
- Stamping punch & die set
- Tread blocks and sipes for tire mold segments
- EDM electrodes for subsequent sinker EDM work
- Custom fixtures for lathes and CNC mills.
- Go/no-go gauges and profile gauges
- Gauge inserts and inspection templates
Electric Discharge Machining Applications in the Aerospace Industry
Aerospace EDM machining
EDM produces various aerospace components from hard, heat-resistant, high-performance metals & alloys, such as Ti-6Al-4V, Ti-17, Inconel, tungsten, and Waspaloy . Electric discharge machining is used for cooling channels in turbines, honeycomb seals, and intricate engine geometries.
EDM in manufacturing aerospace components maintains tolerances in microns, minimizes heat-affected zones, and eliminates work-hardening risks, which are critical for precision and aircraft safety.
Furthermore, EDM complies with safety and quality standards for aerospace manufacturing, including AS9100, SAE AS7116/3 예산 및 MIL-STD-2175 .
- Small, deep, and angled holes on turbine blades
- Fir-tree slot profiles in turbine discs
- Honeycomb seals in jet engine casings
- Fuel nozzle swirlers
- Complex thin-wall airfoils
- Structural sections and complex profiles in landing gear components
- 유압 액추에이터
- 밸브 부품
- Titanium brackets & mounts for satellites
Electric Discharge Machining Applications in Electronics and Semiconductors
In electronics and the semiconductor industry, the need for micro-level components has grown, along with the use of hard materials such as silicon carbide and gallium nitride. EDM can machine heavily doped SiC and GaN. Micro-switches, connectors, sensor housings, test sockets, and probe cards are a few examples.
Because EDM does not involve shear cutting, it preserves the fragile micro-connector geometry of semiconductor components. Consequently, the burr-free machining allows the shaping of fine-pitch electronic components.
- Fine-pitch micro-connector components
- Semiconductor process-equipment fixtures
- Probe card test needles
- Wafer testing parts/ wafer slicing
- MEMS and inkjet printheads
- IC-test sockets
- 스퍼터링 타겟
지금 프로린을 사용해 보세요!
EDM Applications in Defense Manufacturing
EDM applications in electronics
Precision and detailing are crucial in the manufacturing of defense equipment and components, so EDM is used to produce components for missile systems, radars, weapons, and military aircraft. Additionally, EDM is a good choice for precision machining of high-performance alloys that can withstand extreme pressure and heat.
The key reasons why EDM in the manufacturing of defense components is valued are: the ability to shape and profile hardened aerospace alloys, near-zero cutting force & surface integrity, dimensional accuracy, and small-hole drilling.
애플리케이션 예제 :
- Avionics housings and precision connector components
- Gyroscope flexures
- Space-propulsion class hardware
- Aero-engine nozzle-guide-vane
- 미사일 유도 구성 요소
- Precision satellite components
EDM Applications in Hard Materials Machining
As mentioned before, EDM can cut, shape, and drill hard, heat-treated materials (such as cobalt-bonded tungsten carbide, ~ >70 HRC ); the basic requirement is that the workpiece be electrically conductive.
A conventional CNC machining process, such as milling, uses the shear-cutting method and therefore struggles to machine hard materials due to rapid tool wear. But EDM works well as it removes material by controlled electric sparks. Unlike tool-reach issues in milling or drilling, EDM uses an electrode/wires and can drill long, deep holes precisely.
Let’s look at some hard metals/alloys that can be used in the electrical discharge machining process.
소스
Hardness (~ Approx. HRC)
어플리케이션
AISI H13 공구강
45-55
Dies, inserts, complex cavities
D2 공구강
55-62
Punches, dies, profiles
M2 고속철
60-65
Cutting-tools & Dies
Maraging steel (e.g., M300)
50-55
Thin flexures and aerospace parts
인코넬 718
35-50
터빈 부품
니켈 기반 초합금
30–50 +
터빈 블레이드/베인
티타늄 합금(Ti-6Al-4V)
30-40
Aerospace/defense components
Cemented carbide (WC–Co)
> 70
Dies, punches, and tooling
EDM 가공 서비스 Based on Your CAD Design
At Boda, we excel in machining small, intricate, and detailed features for your parts with tolerances as low as ±0.004 mm . We can handle 30+ hard and difficult materials, including tool steels, hardened steels, titanium alloys, Inconel, and carbides.
At our factory, we have wire EDM, Die-sinker EDM, Hole drilling EDM, and micro-EDM equipment that can be used for custom die & mold tooling production and a variety of industrial components. Our EDM services can also deliver a 혼성 접근법 . If workpieces are processable with milling, turning, drilling, or other methods, we combine them with EDM. CNC machining handles fast bulk material removal and accessible geometry. Then, EDM is used for hard, intricate, small, deep, or force-sensitive features.
에 견적을 원하시면 바로 연락주세요 for your EDM machining design, upload your CAD file and specify the requirements. Our engineers will review your design and provide you with an estimation with DFM feedback.
댓글 0
코멘트를 제출 답장을 취소
귀하의 이메일 주소는 공개되지 않습니다. *표시항목은 꼭 기재해 주세요. *
Comment *
이름 *
이메일 *
웹 사이트
다음에 댓글을 달 때이 브라우저에 내 이름, 이메일 및 웹 사이트를 저장하십시오.
댓글 쓰기
당신은 또한 같은 수 있습니다
방전가공: 공정, 재료, 방법 및 비용
2026년 1월 16일
방전가공은 금형, 다이, 펀치, 기어 및 정밀 금속 부품을 생산하는 데 사용됩니다.
와이어 방전가공(EDM)과 싱커 방전가공 기술의 주요 차이점 살펴보기
2023 년 5 월 30 일
와이어 방전가공(Wire EDM)과 싱커 방전가공(Sinker EDM) 기법 비교
지금 바로 부품을 제작하세요
모든 업로드는 안전하고 기밀로 유지됩니다.