
画像タイトル: パンチング vs. レーザーカット
Punching and laser cutting create openings by different mechanisms. Punching shears sheet with a punch and die; laser cutting uses a focused beam and assist gas. Compare the required geometry, material, quantity, edges and downstream operations.
図面に基づいて穴やスロットを製作する必要がありますか? 板金パンチングサービスをタップし、その後、 見積りをご希望の場合 素材、厚さ、数量によって決まります。
パンチ? それは、強力なスタンプを使って金属に形を切り出すようなものです。 レーザー切断? 超集光された光を使って、驚くほど正確に金属を切断します。適切な機種を選ぶことは、ビジネスにとって非常に重要です。
賢明な企業は、間違った方法を選ぶと時間と費用が無駄になることを知っています。小規模なビジネスを運営しているなら、迅速かつ正確に、そして費用を抑えながら物事を進める方法が必要です。
At プロリーンテック、私たちはお客様の部品製造に最適な方法を見つけるのが得意です。お客様がより早く前進できるよう、最適な方法の選択をお手伝いします。どの方法がお客様のニーズに合っているか、ぜひ一緒に考えていきましょう!
パンチングとは?
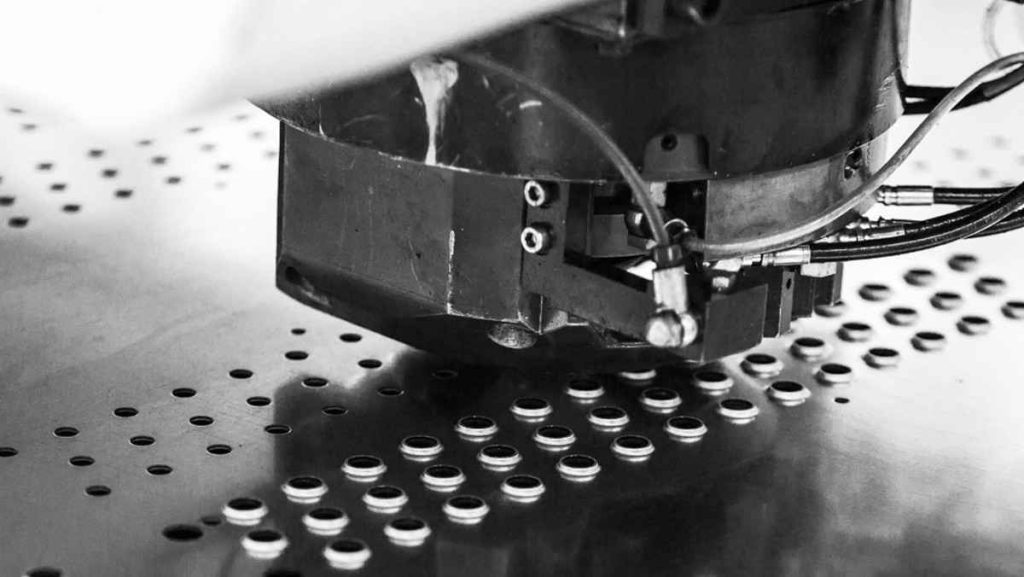
パンチングとは?
パンチング加工は、制御された機械力を用いて金属板から材料を削り出す加工方法です。シートメタルパンチプレスは、硬化鋼製の金型をワークピースに高速で打ち込みます。この加工により、きれいな穴、スロット、複雑な形状を数秒で加工できます。
A punch press drives the punch into the sheet while the die supports it. Deformation, shearing and fracture separate the slug; the penetration at fracture varies with material and clearance.
プレスパンチマシンの構成は、シンプルなシングルステーションユニットから複雑なタレットシステムまで多岐にわたります。タレットプレスは複数の金型を自動で回転させ、手作業による工具交換なしで迅速なパターン作成を可能にします。CNC制御システムは、ワークピースを正確に位置決めし、高い再現性を実現します。
パンチング方式とは何ですか?
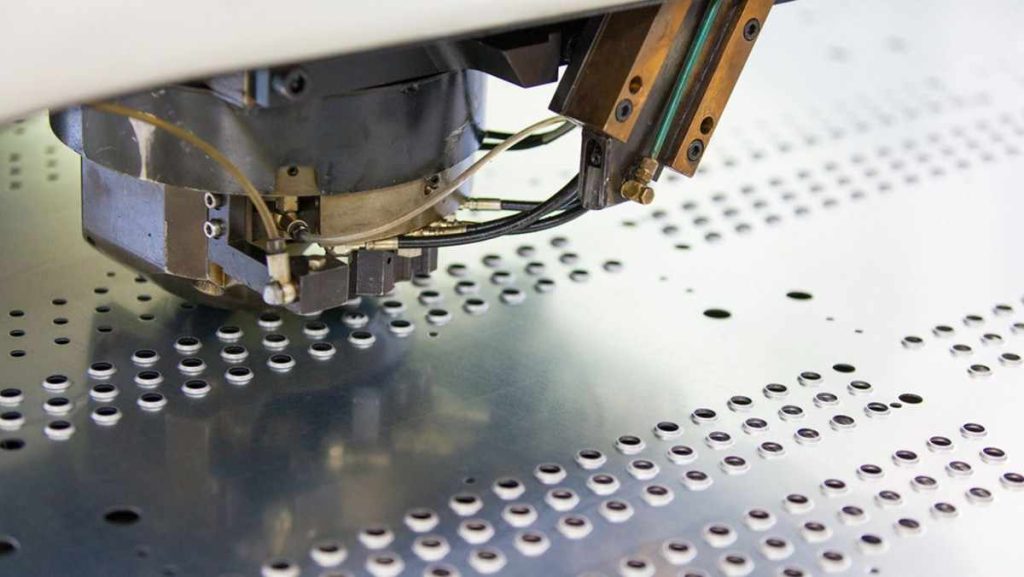
パンチング方式
Punching removes material by shearing. The sheet is positioned relative to the selected tool pair and supported during each stroke; operating rate depends on the machine, material, stroke and part pattern.
パンチングプロセスには 3 つの段階があります。
- 浸透段階: パンチが接触し、材料に入り始める
- せん断段階: パンチが臨界深さに達すると材料が破断する
- 剥離段階: パンチが引っ込み、ストリッパーが材料の付着を防止します。
工具の選定は、穴あけの品質と生産効率を左右します。高速で適切にメンテナンスされたダイは、バリの発生を最小限に抑え、きれいなエッジを実現します。最適な結果を得るには、ダイクリアランス(パンチとダイのクリアランスの差)を材料の厚さと種類に合わせて調整する必要があります。
続きを読む: 板金パンチングの効率化
パンチングの利点は何ですか?
パンチングの利点
パンチング加工には多くの大きな利点があり、一部の作業では最適な選択肢となります。主なメリットは以下のとおりです。
- Repeated holes can make punching worth evaluating when suitable tools are available. Actual throughput depends on tool selection, hit count, sheet movement and material; machine strokes per minute cannot be compared directly with laser travel speed.
- Setup and tooling costs are spread across the order quantity. The total cost still includes sheet utilization, slug and skeleton scrap, deburring, forming and inspection.
- Compatible special tooling can form louvers, embossments or other features on some punch presses. Tool and machine compatibility must be confirmed; these operations are not included automatically in a punching service inquiry.
- Punching is mechanical rather than a thermal cutting process, but force and repeated hits can still distort sheet and create burrs. Specify critical hole dimensions, flatness, edge condition and the final inspection state.
For a part-supply inquiry, review 板金パンチングサービス. Tooling, material, quantity and acceptance requirements are reviewed for the individual project.
パンチのデメリットは何ですか?
パンチのデメリット
プレスとパンチには多くの利点がありますが、考慮すべき制限もいくつかあります。それでは見ていきましょう。
- A nonstandard opening may need special tooling, trials or another cutting route. Compare the quoted tool investment and finished-part price at the actual demand rather than relying on a generic tooling-price range.
- Thickness feasibility depends on material strength, cut perimeter, hole size, tool guidance, clearance and press capacity. Confirm the specific grade and geometry rather than applying a blanket thickness range.
- 打ち抜かれた金属のエッジは必ずしも滑らかではありません。仕上がりは金属の種類と工具の速度によって異なります。金属によってはエッジが粗かったり、ひび割れが生じたりするものがあり、バリ取りなどの追加作業が必要になる場合があります。
- Small-hole feasibility depends on diameter relative to thickness and on the material and tool guidance. Some guided tools can pierce holes smaller than the sheet thickness; this is a tooling-specific capability to assess, not a general guarantee.
レーザー切断とは何ですか?
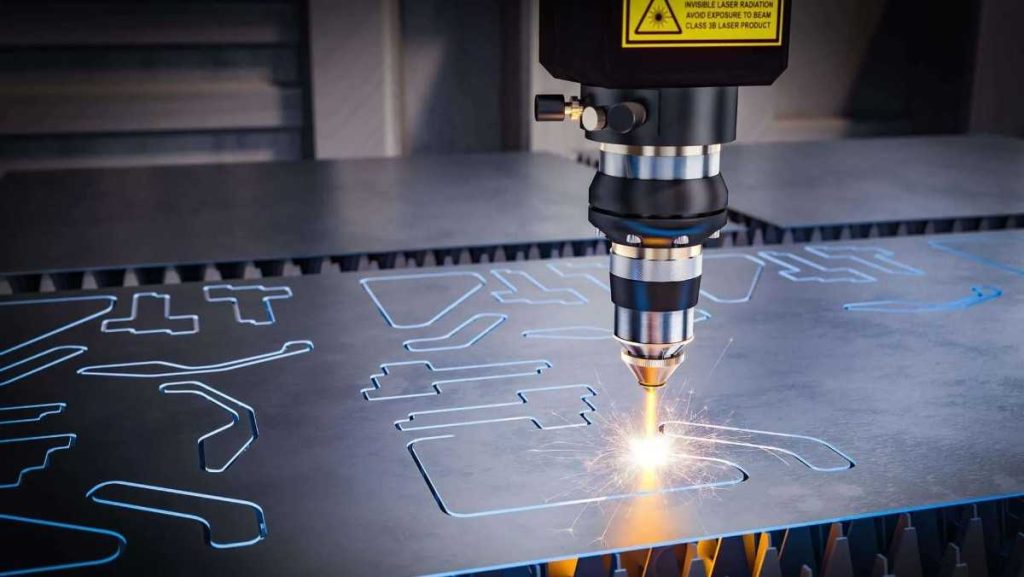
レーザー切断
レーザー切断 強力な集光光を用いて、計画された線に沿って溶解、燃焼、またはガス化を行います。レーザービームは小さすぎるため、高精度な切断は不可能で、周辺部に軽度の熱損傷を引き起こします。
CO2レーザーは通常、板金の切断に使用されます。CO10.6レーザーは波長XNUMXマイクロメートルの赤外線を発します。しかし現在では、ファイバーレーザーの方が切断品質が高く、エネルギー効率が高いことから、人気が高まっています。
切断工程では、複数の処理が同時に行われます。レーザーは金属を溶融またはガス化するまで加熱します。その後、酸素、窒素、空気などの特殊なガスが溶融した金属を切断面から吹き飛ばします。CNC工作機械は、レーザーヘッドを正確な経路で加工し、設計に完全に沿って切断します。
Laser-cutting thickness capacity is machine-, power-, material- and quality-specific. Specify the alloy, thickness and edge requirements for a feasibility review.
今すぐプロリアンをお試しください!
レーザー切断プロセスを理解する
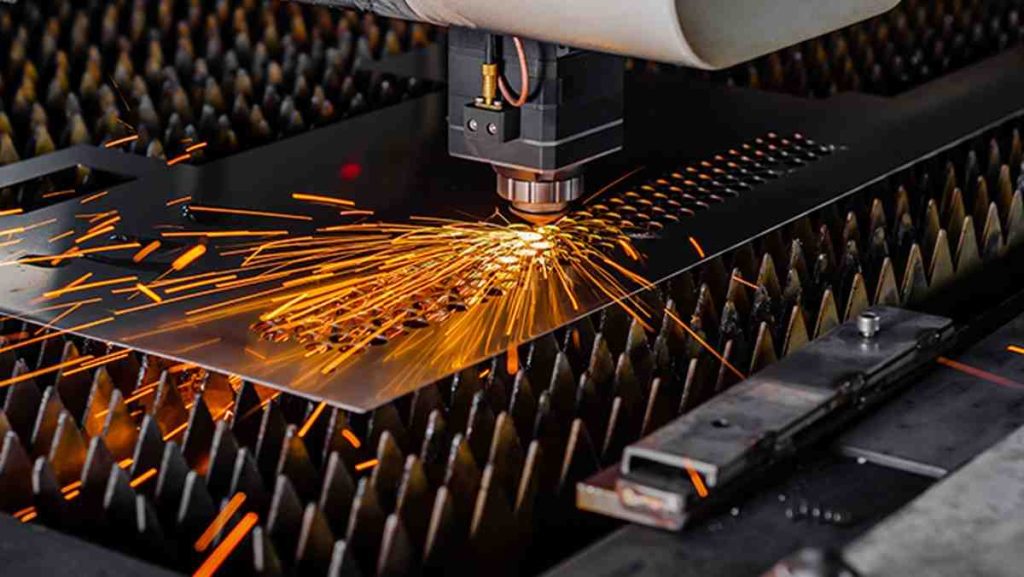
レーザー切断プロセス
レーザー切断は、コンピュータ支援設計(CAD)ファイルの準備から始まります。ネスティングソフトウェアは、シート材料上に部品を最適に配置し、無駄を最小限に抑えます。CNCプログラミングは、形状を機械が読み取り可能な命令に変換します。
Beam delivery and focusing optics direct laser energy to the cut. Focus settings and beam characteristics depend on the laser source, head, material and thickness.
The motion system follows the programmed contour. Positioning specifications alone do not establish finished-part tolerance, which also depends on the cut process, material and measurement conditions.
プロセス監視 一貫した切断品質を確保します。センサーが切断面の通過を検知し、アシストガスの圧力を監視し、ビームの位置合わせを行います。自動高さ制御により、材料の厚さが変化しても最適な焦点位置を維持します。
レーザー切断の利点は何ですか?
レーザー切断の利点
レーザー切断は、高い精度ときれいな仕上がりで知られています。現代の製造業に多くのメリットをもたらします。詳しく見ていきましょう。
- Laser cutting can follow detailed contours without a shape-specific cutting die. Achievable tolerances, kerf, taper and edge quality depend on the machine, material, geometry and process settings.
- CAD and program changes can support design revisions without a new shape-specific cutting die. Programming, material, setup and sample approval still affect the schedule.
- Laser compatibility depends on the source, material and cutting system. This comparison concerns metal sheet; plastics, ceramics and composites require a separate compatibility and safety review.
- Laser-cut edges may need dross removal, oxide removal or other finishing depending on material, assist gas and acceptance criteria. The heat-affected edge and any taper must be considered.
- Laser cutting avoids wear on a contacting shape-specific cutting die, but optics, nozzles, protective windows and the cutting system still need maintenance.
レーザー切断の主な欠点は何ですか?
レーザー切断の欠点
レーザーカッティングは精度の高さで知られていますが、いくつかの欠点も存在します。これらの問題は、製造時間、コスト、そして材料の選択肢に影響を与える可能性があります。
- Relative throughput depends on geometry, hole count, sheet movement, laser cutting conditions, tool selection and secondary work. Neither route is always faster.
- レーザーカッターは、電力消費量が多く、定期的なメンテナンスも必要となるため、コストが高くなります。レーザー管、レンズ、ミラーなどの部品は摩耗するため、交換が必要です。窒素や酸素などの補助ガスの使用もコストを増加させます。適切なレーザー加工機の種類を選択することで、ランニングコストを大幅に削減できます。
- レーザーカッターは、材料の厚さにも制限があります。この制限は、レーザーの出力と金属の種類によって異なります。アルミニウムや銅などの光沢のある材料はレーザービームを反射するため、切断が困難になります。厚い材料を適切に切断するには、追加のパスや特別な装置が必要になる場合があります。
- もう一つの問題は、切断中に発生する熱です。この熱はエッジ付近の金属を置換し、部品の動作に影響を与える可能性があります。プロジェクトによっては、熱の影響を受けやすい部分を洗浄または修復するための追加工程が必要になる場合があります。
切断と打ち抜きの違いとは? – 比較表
切断と打ち抜きの違い
パンチングとレーザー切断の主な違いは、材料を除去する方法と、残すタイプです。
パンチング加工は、強力な機械力を用いて金属を削り出し、材料をせん断することで切断します。これにより、滑らかな部分と粗い部分の両方を持つ特殊なエッジが形成されます。スラグと呼ばれる金属片は、メインシートから完全に押し出されます。
切断、特にレーザーによる切断は、熱を用いて金属を除去します。レーザーは切断線に沿って金属を溶融またはガス化します。これにより、カーフと呼ばれる滑らかで狭い切断面が形成され、熱の影響を受けたエッジが解放されます。パンチングとは異なり、レーザーは材料を流れるように除去するため、パンチングでは不可能な複雑な形状にも対応できます。
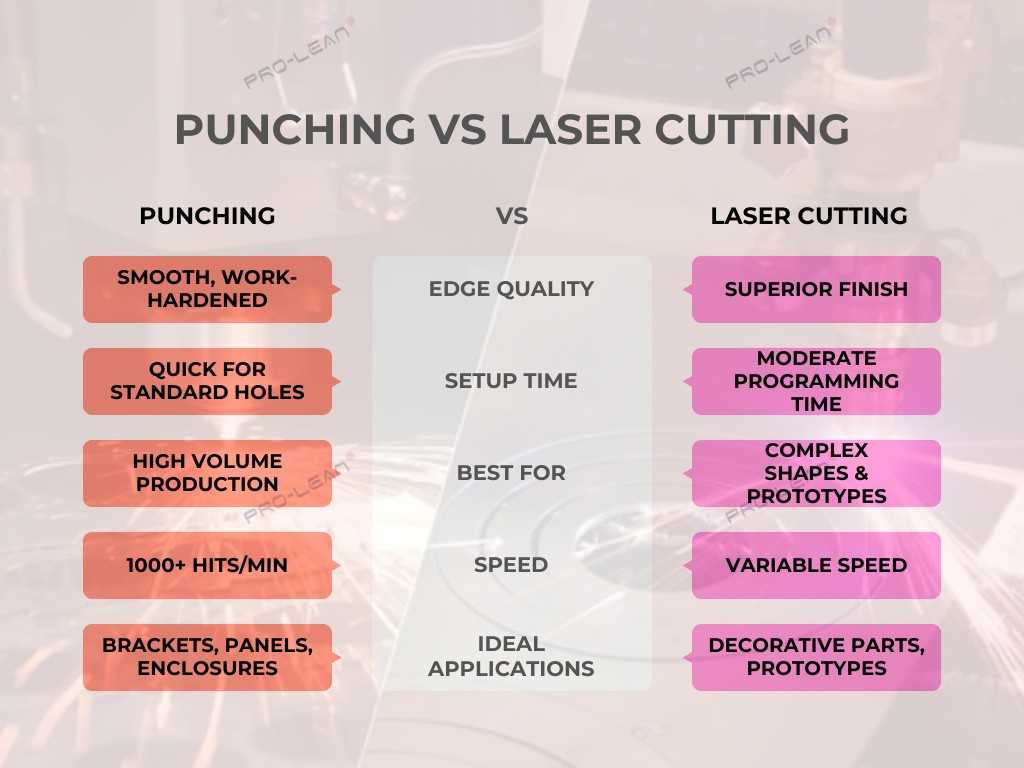
画像タイトル: パンチング vs レーザーカットインフォグラフィック
以下はパンチングとレーザーカットの比較表です。
| 決定要因 | 打ち抜き | レーザー切断 |
|---|---|---|
| 切断機構 | Mechanical shearing with a matched punch and die | Thermal cutting using a focused beam and assist gas |
| ジオメトリ | Tool-defined holes, slots and repeat patterns | Programmed profiles and openings within process limits |
| ツーリング | Existing shape tools or special tooling | No shape-specific cutting die; programming and setup remain |
| 数量とコスト | Review tool investment, hits, nesting and secondary work | Review cutting time, gas, nesting and secondary work |
| Accuracy and capacity | Confirm for grade, thickness, geometry, tooling and inspection | Confirm for grade, thickness, geometry, machine and inspection |
| エッジと平面度 | Rollover, fracture, burr and mechanical distortion need review | Kerf, taper, dross, oxide and thermal effects need review |
製造の観点から見ると、パンチング加工は穴や単純な形状などの個別の機能を高速で作成するのに優れており、一方、切断加工は複雑な輪郭や入り組んだ詳細に対して優れた幾何学的柔軟性を提供します。
今すぐプロリアンをお試しください!
パンチング vs レーザーカット、どちらを選ぶべきでしょうか?
レーザー切断とパンチング、どちらを選ぶべきでしょうか?
パンチと 右レーザーカッター プロジェクトのニーズによって異なります。ボリューム、サイズの複雑さ、材料の種類、全体的なコストなどが重要な役割を果たします。
1. 生産量
Repeated demand can justify tool investment, but there is no universal order-quantity cutoff between punching and laser cutting. Compare the actual pattern and finished-part cost at the requested quantities.
2. サイズとデザインに基づいて
部品のサイズも重要です。パンチングはシンプルな穴や基本的な形状に最適です。複雑な線や細かいディテール、あるいは高い精度が求められるデザインの場合は、レーザーカットの方が適しています。
3. 材質の種類
Review the exact alloy, thickness, surface condition and required features for both routes. Reflectivity and thermal behavior affect laser process selection; strength, geometry and tooling affect punching.
4. コストと効率性に基づいて
最適な価値を見つけるには、機械の稼働時間だけでなく、総コストも考慮してください。パンチング加工には特殊な機材が必要になる場合があり、セットアップにも時間がかかります。レーザーカットは加工速度は遅くなりますが、追加工程は少なくて済みます。最適な選択肢は、お客様の作業の具体的な要件によって異なります。
その時点で、Boda の専門家がプロジェクトのニーズに応じて適切な切断方法を決定するお手伝いをいたします。
カットとスマッシュカットの違いは何ですか?
カットとスマッシュカットの違い
切断作業では材料を完全に削り取り、穴や仕切りを作ります。パンチングとレーザー切断はどちらも金属片から材料を除去するため、純粋な切断方法です。
“Smash cut” is not a useful specification for selecting a sheet-metal manufacturing route. Specify a pierced opening, blanked profile, lanced tab or formed feature on the drawing instead.
Cutting and forming change a part in different ways. Assess edges, remaining section, loads and any deformation for the actual design; neither a cutting label nor a forming label establishes component strength.
業界リーダーのための高度な金属加工ソリューション
今日の工場では、パンチング加工とレーザー切断の両方が必要となることがよくあります。多様な顧客のニーズに応えるため、賢明なメーカーは複数の方法を活用しています。これにより、あらゆる種類の注文に、より迅速かつ効率的に対応できます。
1. パンチとレーザーを併用する
両方の手法を組み合わせて使用している企業もあります。まず、パンチング加工で一般的な形状や穴を素早く加工し、次にレーザーカットで幅広や複雑なデザインを加工します。このスマートな組み合わせにより、時間を節約し、選択肢を広げることができます。
2. 他のプロセスとの接続
これらの切断方法は単独で機能するものではなく、曲げ、溶接、表面仕上げを含む大規模なシステムの一部です。例えば、最初にパンチング加工を行い、その後レーザー切断で滑らかな仕上げを施すことができます。これにより、単独では実現できない形状を実現できます。
3. 高い品質を維持する
優れた企業は、どちらの切断方法においても品質チェックを実施しています。統計的工程管理(SPC)などのシステムを用いて、パンチング加工やレーザー切断時の主要な設定値を把握しています。これにより、問題を迅速に解決し、すべての部品を要件通りに維持することができます。
4. 適切なテクノロジーの選択が重要
の専門家 板金パンチングBodaのような企業は、適切な方法を選択することが生産プロセス全体に影響することを熟知しています。重要なのは、単に切断するだけでなく、すべてがスムーズに連携して機能することです。
プロレアンテックの 板金穴あけ 専門家は、テクノロジーの選択が制作ワークフロー全体に影響を及ぼすことを理解しています。
Boda を選ぶ理由
Boda を選ぶ理由
レビュー 板金パンチングサービス for hole- and slot-focused parts, or レーザー切断サービス for a programmable contour route. The drawing, material, demand and acceptance requirements determine the project scope.
経験豊富なチームが、お客様のニーズに最適なプロセスの選択をお手伝いします。お客様のデザインを綿密に調査し、最もコスト削減効果の高い方法をご提案いたします。この専門的なアドバイスにより、あらゆるプロジェクトにおいて時間とコストの節約を実現いたします。
Agree critical dimensions, edge condition, flatness, inspection methods and documents in the quotation. A quality-management-system certificate does not guarantee every part or establish a universal product tolerance.
If samples are needed, define their purpose, quantity and acceptance criteria. Confirm the sample route and schedule separately from repeat-production requirements.
結論 – パンチング vs レーザーカッティング
Punching merits evaluation for repeated tool-defined holes and patterns. Laser cutting merits evaluation for flexible contours and changing geometry. Compare tooling, finished-part cost, edge condition, flatness and downstream work; neither route has a universal accuracy, cost or speed advantage.
最適な方法は、必要な部品の数、サイズの複雑さ、そして予算によって異なります。多くの賢明なメーカーは、作業内容に応じて両方の方法を使い分けています。パンチングとレーザーカットを組み合わせることで、最良の結果が得られます。
Send the drawing, material, quantity and critical requirements through the 引用ページ so the proposed route and secondary operations can be reviewed together.
見積もりを取得 今日!
よくあるご質問
レーザー切断と比較したパンチングの利点は何ですか?
Repeated openings may favor punching where appropriate tools and sequence reduce the total cost. Mechanical punching avoids a thermal cut but can still cause burrs, local work hardening and distortion. The decision requires the actual part and quantity.
パンチカットのメリットは何ですか?
Punching creates repeatable tool-defined openings, but the sheared edge can include rollover, burnish, fracture and an exit burr. Sheet deformation and any deburring requirements must be assessed for the finished part.
パンチングとカッティングのプロセスとは何ですか?
The sheet is positioned and supported between a punch and die. The punch deforms and shears the material, the slug separates, and the tool retracts while stripping releases the sheet. Fracture depth depends on material and tooling clearance.